
The First Line of Defense: Why a Coarse Disc Filter Extends the Life of Industrial Reverse Osmosis
Protecting industrial reverse osmosis membranes and pumps: why a coarse disc filter is more effective than Big Blue cartridges and how to properly assemble the unit.
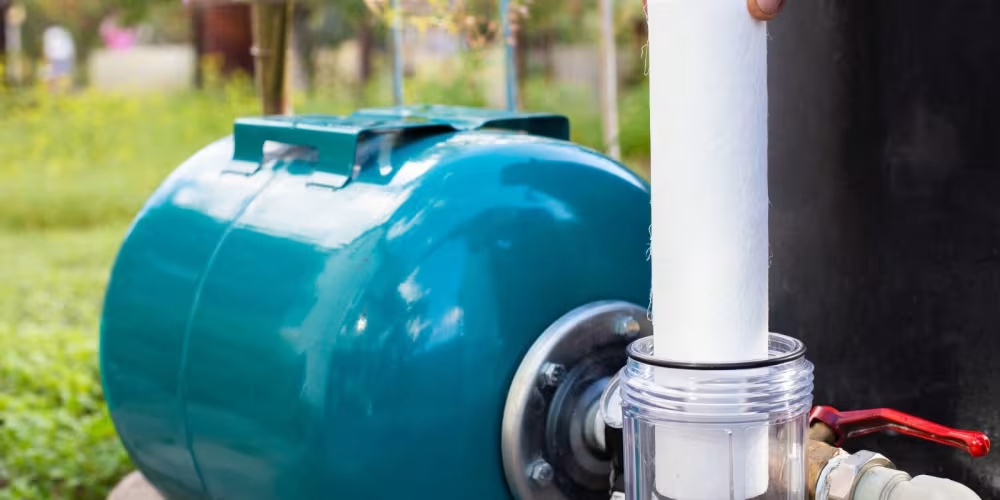
In industrial water treatment, membrane desalination is rightfully considered the pinnacle of engineering technology. High-capacity commercial and industrial systems are capable of removing up to ninety-nine percent of dissolved salts, producing ultrapure water for steam boilers, chemical production, food processing lines, and pharmaceuticals. However, this impeccable filtrate quality comes at a high technological price: the heart of the system—polyamide spiral-wound elements and high-pressure plunger pumps—is extremely vulnerable to mechanical impurities in the incoming flow.
If the water flow brings along a sudden surge of sand from an artesian well or flakes of scale from a worn-out municipal water supply, expensive equipment is immediately threatened with emergency shutdown. For many years, engineers relied solely on disposable fine cartridge filter housings, but in practice, those instantly "choke" under peak loads. This is precisely why a disc water filter installed as an uncompromising primary line of defense has become the modern standard of reliability.
Let's examine the hydraulic and mechanical risks faced by industrial osmotic stations, why flat meshes and thin cartridges cannot withstand overloads, and how disc technology repeatedly extends the lifespan of membranes and pumping units.
Hidden Threats to Osmosis: Abrasives, Spacers, and Water Hammers
To appreciate the importance of the first line of defense, we need to look at the vulnerable components of a reverse osmosis system through the lens of hydrodynamics.
The high-pressure pump is the first to take the hit from suspended particles. Whether it is a multistage vertical centrifugal unit or a plunger pump creating a working pressure of ten to twenty-five bar in the system, its impellers and seals rotate at immense speeds. Hard particles of quartz sand and metal scale act like abrasive sandpaper. Within a few weeks, they wear down the mechanical graphite seals, cut the edges of the blades, and lead to cavitation wear in the flow-through section. The result is a loss of head, motor overheating, and thousands of dollars in major pump repairs.
The second critical zone is the inlet channels of the membrane block. Inside the composite roll, between the layers of the polyamide sheet, lies a thin polymer mesh turbulator called a spacer. The thickness of these channels is a fraction of a millimeter. If suspended mechanical particles break through the pretreatment, they become firmly wedged in the spacer cells at the frontal face of the first membrane element in the housing.
The free cross-section for water flow is blocked, hydrodynamic resistance rises sharply, and the flow begins to push against the ends of the roll. In engineering, this phenomenon is called telescoping: under the influence of pressure drop, the internal layers of the membrane shift relative to the central permeate tube, the outer protective shell ruptures, and the expensive element turns into a piece of deformed plastic.
The Weakness of Cartridge Pre-Filters: Why "20 Big Blue Housings" Fall Short
The classical commercial osmosis scheme often includes a fine cartridge filter with replaceable elements made of blown polypropylene with a 5-micron rating. Engineers often assume that this specific cartridge will handle all the mechanical debris. However, in real industrial conditions, such a solution without a prior heavy-duty barrier turns into a financial black hole.
A polypropylene cartridge has limited surface and pore capacity. When drawing water from wells with fluctuating sand yields or seasonal turbidity variations in water bodies, a 5-micron cartridge clogs within a matter of hours.
When the polypropylene pores become blocked by silt and rust, the pressure drop across the housing rises sharply. If the operator fails to replace the element in time, two typical failures occur: either the station automation shuts down the pump due to dry running, paralyzing the entire production workshop, or the soft polypropylene core flattens and ruptures under the incoming water pressure. At the moment of the rupture, the dense mass of dirt accumulated over days of operation flies straight into the working stages of the high-pressure pump and clogs the membrane rolls in a single surge.
This is precisely why a reliable heavy-duty disc water filtration filter must be installed upstream of the fine microfiltration unit, taking the brunt of large and medium suspended solids.
The Physics of the Volumetric Trap: How the Disc Stack Operates Under Load
The fundamental advantage provided by a disc water filter lies in the geometry of the filtering medium. Unlike a flat mesh, where filtration occurs in a single plane and particles instantly blind the openings, the disc stack operates on the principle of a spatial three-dimensional matrix.
Plastic discs made of virgin polypropylene feature microscopic grooves and channels of a specific depth on their surface, angled against each other. When compressed into a tight stack by a spring and incoming water pressure, they form not a sieve, but a continuous volumetric labyrinth.
When water saturated with rust particles, sand grains, and scale flakes passes from the outside to the inside of the stack, the sludge distribution occurs throughout the entire thickness: large grains of sand and heavy scale are intercepted at the outer contour of the discs. Finer fractions, colloidal silt, and clay particles penetrate deeper into the narrowing intersecting channels and settle in special trap cavities. Thanks to this, a disc water filter possesses colossal dirt-holding capacity, exceeding the performance of mesh alternatives by four to six times.
Even during intensive well sanding, the outlet pressure from the filter remains stable. The system reliably "shears off" mechanical peaks, passing only optically clear water with residual micro-suspended solids further to the fine five-micron stage. The service life of replaceable cartridges increases four to five times, and the membrane rolls remain completely safe.
The Economics of Trouble-Free Operation: Calculating Enterprise Costs
For a workshop manager or chief engineer, the integration of any unit into a water treatment scheme is always measured in figures of operational expenses and prevented damages.
Let's look at the basic economics of a commercial osmotic system with a capacity of five cubic meters of permeate per hour, equipped with four industrial-standard membranes:
Replacing a set of four high-rejection membrane elements after a mechanical failure costs approximately 45,000 to 60,000 hryvnias each.
Overhauling stages or purchasing a new stainless steel high-pressure pump requires another 35,000 to 70,000 hryvnias.
Technological downtime of a food processing line, beverage bottling plant, or boiler room while waiting for component delivery and housing flushing is often measured in hundreds of thousands of hryvnias in lost profit.
Against this backdrop, the cost of timely purchasing a disc water filtration filter with manual or semi-automatic flushing accounts for a minuscule fraction of the main equipment's cost, depending on the connection diameter and flow capacity. High-quality polypropylene disc water filters do not require purchasing replacement consumables: the discs are corrosion-resistant, do not wear out from quartz sand impacts, and can be cleaned in a minute with a water jet, lasting over seven to ten years. The investment in such a protection unit pays off during the very first water hammer in the pipeline or sudden surge of sand from a well.
Integration Subtleties: How to Properly Build the Unit Into the Line
For disc mechanical filtration to operate with maximum efficiency, the design piping must account for several engineering rules:
Installation strictly upstream of the booster pump: The protective filter is mounted at the station inlet—ahead of the high-pressure pumps, antiscalant dosing units, and fine cartridges.
Selection of the filtration rating: The gold standard for the pretreatment stage before industrial osmosis is a micron rating of 100–130 microns (yellow or red marked discs). This pore size perfectly intercepts all abrasive sand and formation dirt without creating excessive hydraulic resistance on the pump suction line.
Monitoring pressure drop via pressure gauges: It is recommended to install two pressure gauges—before and after the disc filter. A pressure drop exceeding 0.6–0.8 bar serves as an unmistakable signal to the operator that routine flushing of the stack is required.
Summary
Industrial reverse osmosis is a high-precision and capital-intensive investment requiring a professional approach to every water treatment unit. Trying to save money on the first stage of mechanical purification by shifting this task to fine cartridges or meshes inevitably leads to failures, abrasive pump wear, and the premature death of expensive spiral-wound membranes.
Modern disc water filters create an unbreakable shield at the system inlet. By protecting the technological pathway from peak mechanical overloads, sand, and scale, they ensure trouble-free equipment operation, reduce maintenance time, and guarantee the stable production of crystal-clear water for your business every day.
Editorial team agronom.info
Materials are prepared by the portal's agronomists and editors. We use only trusted sources: Ukrainian agricultural universities, variety registries, open scientific publications.
Related articles
Not yet comments. Be the first!
Comments